EN
Quick Links

Whether transmitting 30 MHz ultrasound echoes, supplying high-definition signals from a camera-based scope, or delivering power to a high-frequency RF ablation probe, coaxial cables must maintain consistent performance throughout their service life. Their design ensures the correct impedance, low attenuation, and stable phase response across the entire intended bandwidth. Even relatively small impedance discontinuities or increases in attenuation can affect signal integrity in sensitive high-frequency applications, depending on the system design and operating bandwidth..
Consistent RF performance in a high-frequency coaxial cable depends on controlling the complete transmission structure, not on any single material or component.
The most important design controls typically include conductor and dielectric geometry, characteristic impedance, shielding structure, cable termination, connector transitions, environmental stability, and manufacturing consistency.
If → conductor and dielectric dimensions vary beyond the design tolerance
Then → impedance and other RF characteristics may change
Why → the physical geometry of a coaxial transmission line directly affects its electrical behavior.
If → shielding construction or shield termination is inconsistent
Then → evaluate shielding continuity and the complete return path
Why → the shield forms part of the RF transmission structure and EMI control system.
If → cable termination introduces a geometry change
Then → control strip length, dielectric position, conductor alignment and connector termination
Why → the transition between cable and connector can introduce an electrical discontinuity.
If → the cable operates under temperature, humidity or repeated-flex conditions
Then → validate RF performance under representative environmental and mechanical conditions
Why → a cable that meets its initial specification may behave differently after environmental or mechanical stress.
For controlled RF transmission, see HOTTEN's RF Cable.
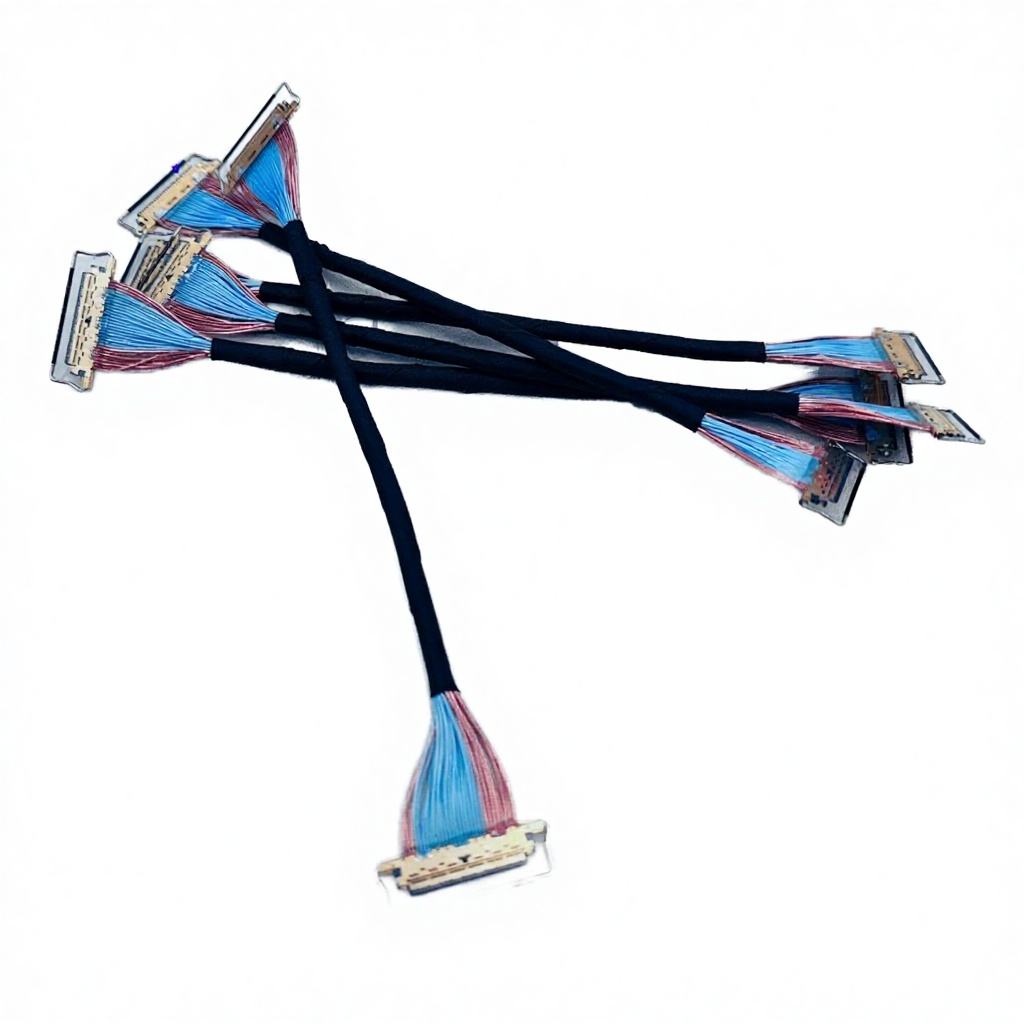
For complete terminated solutions, see RF Coaxial Cable Assembly.
Precision Dielectric Extrusion and Dimensional Tolerances
The electrical characteristics of a coaxial cable are determined by the relationship between the conductor diameter and dielectric insulation. Tolerances of up to 2% in either element can alter the characteristic impedance of a cable by up to two ohms and contribute to reflections and return loss. We use a precisely controlled extrusion facility that utilizes in-line real-time diameter feedback to control the concentricity and thickness of the PTFE and e-PTFE insulators to 2 percent tolerances. Our ICE and IVUS applications use e-PTFE, which has a low relative permittivity (εr ≈ 2.1) across frequencies from DC to 1 GHz.
Shield Construction and Transfer Impedance Minimization
Transfer impedance measures how effectively a coaxial cable prevents external RFI from entering the cable and internal signals from leaking out, and is typically expressed in ohms per meter (mΩ/m). For effective RFI and EMI shielding above 1 MHz, a shield with more than 95% coverage is typically required. This usually involves a double-shielded configuration, such as a foil layer combined with a tinned copper braid, for high-frequency surgical applications.
For RF ablation applications operating at 400–500 kHz, we use an additional semiconductive layer beneath the foil shield to reduce the risk of creepage.. The silver plating on the braid helps reduce surface resistance at the higher frequencies and provides a transfer impedance of under 5 mΩ/m.
Controlled Cable Assembly and Termination Techniques
Our team of highly skilled cable technicians at Hotten adheres to strict termination procedures to minimize the impact of the termination on overall cable performance. This includes precise control of conductor strip length and insulation clearances to within 0.008 inches, optimized solder temperature profiles to prevent dielectric degradation and properly controlled crimp compression on contacts which are confirmed through crimp quality is verified through pull testing against application-specific requirements. Our automated semi-rigid assembly machines precisely strip, align, solder and terminate cables. Automated inspection systems verify each connection to ensure that conductor position within the termination connector is perfectly centered and the dielectric surface is flush.
For an OEM project, RF consistency should be evaluated as a chain of controlled variables.
A practical framework is:
Geometry → Impedance → Shielding → Termination → Environment → Testing → Production Consistency
A cable that performs well during initial testing still needs to demonstrate that these parameters can be controlled repeatedly during production.
Before defining manufacturing controls, engineers should first establish the required electrical performance.
Typical requirements may include:
| Parameter | Engineering Question |
|---|---|
| Frequency | What is the operating frequency range? |
| Impedance | 50Ω, 75Ω, or another system requirement? |
| Attenuation | What is the maximum acceptable loss? |
| Return loss / VSWR | How much mismatch can the system tolerate? |
| Phase stability | Is phase consistency important? |
| Cable length | What finished length is required? |
| Capacitance | Is cable capacitance a system constraint? |
| Shielding | What level of EMI/RFI control is required? |
If → the application has a clearly defined RF performance window
Then → convert those requirements into cable geometry and process controls
Why → manufacturing controls should exist to protect actual system requirements.
If → no clear electrical acceptance criteria have been defined
Then → establish the required RF parameters before setting detailed production tolerances
Why → otherwise, the supplier may optimize dimensions without knowing which electrical characteristics are actually critical.
For impedance-focused engineering, see How Impedance Control Helps High-Frequency Coaxial Cable Maintain Stable Signal Transmission.
Characteristic impedance is determined by the physical relationship between the conductor, dielectric and surrounding conductive structure.
Important dimensional variables can include:
If → conductor and dielectric geometry are stable
Then → the transmission structure is easier to keep within the required impedance range
Why → dimensional consistency supports electrical consistency.
If → dimensional variation is concentrated in one section of the cable
Then → investigate whether the local geometry creates an impedance discontinuity
Why → RF performance is affected by the actual transmission path, not just average cable dimensions.
The existing HOTTEN article already emphasizes precision dielectric extrusion and control of conductor/dielectric geometry as a core design factor.
A cable may pass an impedance test at one stage, but OEM engineers should also consider where and how the impedance is controlled.
A useful process is:
Conductor Geometry
→ Dielectric Geometry
→ Shield Structure
→ Cable Assembly
→ Connector Transition
→ Finished Cable Test
If → the cable construction is dimensionally consistent but the connector transition is poorly controlled
Then → the finished assembly may still require investigation
Why → the connector and termination become part of the signal path.
This is why finished-assembly testing can be more informative than relying only on raw cable measurements.
Shielding is not simply a specification such as:
“Use double shielding.”
The engineering question is:
Can the selected shielding structure be produced consistently and terminated consistently?
Relevant factors include:
| Shielding Factor | Engineering Consideration |
|---|---|
| Shield material | Electrical and mechanical properties |
| Shield construction | Foil, braid, combination, etc. |
| Coverage | EMI/RFI control requirement |
| Shield continuity | Complete electrical path |
| Shield termination | Connection to connector/ground structure |
| Flexibility | Effect of repeated bending |
| Cable OD | Impact on device integration |
| Process consistency | Repeatability in production |
If → EMI/RFI performance is critical
Then → specify the required shielding structure and validation method
Why → shielding requirements need measurable acceptance criteria.
If → the cable must also be very flexible
Then → evaluate shielding structure together with bend requirements
Why → a shielding construction can affect overall cable stiffness and mechanical behavior.
HOTTEN's current article already discusses foil and braided shielding as part of its RF cable construction strategy.
For application-level RF solutions, see High Frequency & RF Systems.
The cable may have excellent RF characteristics before termination, but the finished assembly also contains:
Conductor → Dielectric → Shield → Termination → Connector
The termination area should therefore be considered part of RF design.
Important controls may include:
If → the termination changes the physical geometry of the coaxial structure
Then → inspect and validate the transition
Why → an abrupt geometry change can affect the RF path.
If → the assembly uses different connectors for different applications
Then → validate each cable/connector combination separately
Why → connector geometry and termination conditions are application-specific.
The HOTTEN article already identifies strip length, insulation clearance, solder profile, crimp compression and automated inspection as termination controls.
For finished assemblies, see RF Coaxial Cable Assembly.
RF consistency is not only a room-temperature laboratory issue.
Depending on the application, engineers may need to evaluate:
If → the cable operates in a temperature-variable environment
Then → validate RF characteristics across the required temperature range
Why → material properties and cable geometry can change with environmental conditions.
If → the cable experiences repeated bending
Then → evaluate electrical performance before and after representative mechanical testing
Why → mechanical deformation can affect the physical transmission structure.
The current article describes environmental cycling and flex-related measurements as part of HOTTEN's validation approach.
For mechanical/electrical trade-offs, see How to Balance Mechanical and Electrical Performance in Ultra-Fine Coaxial Cables.
An important manufacturing distinction is:
Inspection detects variation; process control is intended to prevent excessive variation.
For high-frequency coaxial cables, useful controls can occur throughout production:
| Manufacturing Stage | Example Control |
|---|---|
| Conductor preparation | Conductor dimensions / surface condition |
| Dielectric extrusion | Diameter / concentricity / thickness |
| Shielding | Coverage / continuity / construction |
| Cable cutting | Length |
| Stripping | Strip length |
| Termination | Conductor and dielectric position |
| Connector assembly | Alignment / insertion |
| Final testing | Impedance / attenuation / continuity |
| Environmental validation | Temperature / humidity / flex response |
If → final testing finds repeated failures at the same stage
Then → investigate the upstream manufacturing process
Why → correcting the final product without correcting the process does not improve process capability.
When an OEM project moves from prototype to volume production, the question changes from:
“Can you make this cable?”
to:
“Can you make this cable consistently?”
That means engineers should pay attention to:
If → prototype samples meet the required RF performance
Then → evaluate whether the same controls can be maintained across production lots
Why → a few successful samples do not by themselves demonstrate production consistency.
If → a critical parameter depends heavily on manual adjustment
Then → evaluate whether the process can be standardized or automated
Why → process dependence on individual adjustment can create additional production variation.
There should not be one identical validation program for every coaxial cable.
If → the cable is used in ultrasound, ICE, IVUS or another medical imaging system
Then → evaluate RF performance together with compact geometry, flexibility and the application's environmental requirements
Why → medical cable assemblies can combine electrical, mechanical and environmental constraints.
See Medical Equipment.
If → the cable is used in an RF ablation system
Then → evaluate electrical performance, insulation structure, shielding and the relevant environmental/mechanical conditions together
Why → the cable design must match the specific electrical and safety requirements of the equipment.
See RF Ablation Cable.
If → the cable is installed in a moving UAV, gimbal or robotic system
Then → combine RF testing with flex and vibration-related validation
Why → a cable may need to maintain signal performance while experiencing repeated mechanical movement.
See UAV & Robotics.
A useful RFQ should describe both performance requirements and manufacturing acceptance criteria.
| Category | Recommended Information |
|---|---|
| Frequency | Operating frequency range |
| Impedance | 50Ω / 75Ω / other |
| Attenuation | Maximum acceptable value |
| Return loss / VSWR | Required limit if applicable |
| Phase | Stability requirement if applicable |
| Cable length | Nominal + tolerance |
| Cable OD | Maximum allowable dimension |
| Conductor | Material / size / construction |
| Dielectric | Material / structure |
| Shielding | Structure / coverage / termination |
| Connector | Part number / interface |
| Termination | Solder / crimp / other |
| Environmental | Temperature / humidity / chemicals |
| Flexibility | Static / dynamic |
| Testing | Electrical + mechanical + environmental |
| Production | Prototype / pilot / mass production |
If → the RFQ only states “50Ω low-loss coaxial cable”
Then → add frequency, attenuation, cable length, connector and environmental requirements
Why → otherwise different cable constructions may satisfy the same general description.
A useful design sequence is:
System Requirement
→ Frequency
→ Impedance
→ Attenuation / Return Loss
→ Conductor + Dielectric Geometry
→ Shielding
→ Termination
→ Environmental Requirements
→ Prototype Testing
→ Production Process Validation
→ Final Assembly Testing
For a medical high-frequency cable, for example:
Medical imaging requirement
→ determine frequency range
→ define impedance
→ determine acceptable attenuation
→ define cable diameter
→ select conductor and dielectric
→ select shielding structure
→ define connector and termination
→ test initial RF performance
→ perform representative mechanical/environmental validation
→ verify production consistency.
This creates a much stronger engineering chain than simply specifying:
High-Frequency Coaxial Cable + 50Ω
Why Choose Silver-Plated Conductors for High-Frequency Signal Transmission Cables?
How RF Coaxial Cable Assemblies Control Impedance and Loss for Reliable High-Frequency Signals
How Impedance Control Helps High-Frequency Coaxial Cable Maintain Stable Signal Transmission
How Material Selection and Strain Relief Extend RF Coaxial Cable Assembly Service Life
How to Balance Mechanical and Electrical Performance in Ultra-Fine Coaxial Cables
Environmental Stability—Temperature, Humidity, and Flex Effects
An otherwise perfectly manufactured coaxial cable assembly could still exhibit inconsistent performance in temperature-variable or humid clinical environments or after extensive flexing. We subject many designs to 96-hour thermal/humidity cycling (40°C, 95% RH), monitoring impedance and attenuation variations, and measure phase shift under flex conditions using robotic and camera-based test fixtures. Our materials are chosen to withstand significant temperature and humidity variations and offer a low coefficient of thermal expansion, such as FEP and ETFE jacketing which are hydrophobic and resist moisture absorption.
Conclusion
Delivering a high-performance, highly reliable coaxial cable is the result of the precise control of all four of these design factors. At Hotten’s modern manufacturing facility we have built extensive design, engineering and manufacturing capabilities across 10,000 square meters to develop and build over 300 unique cable specifications per year.
Whether a surgeon needs a perfectly controlled RF ablation signal or a diagnostic probe that provides the clearest image available, Hotten’s coaxial cable technology provides reliable and consistent performance across demanding applications.
 Hot News
2026-09-17
2026-09-04
2025-12-17
2025-12-11
2025-12-05